Left Is a Decision, Not a Default: Fixing Orientation on Handed Metalwork
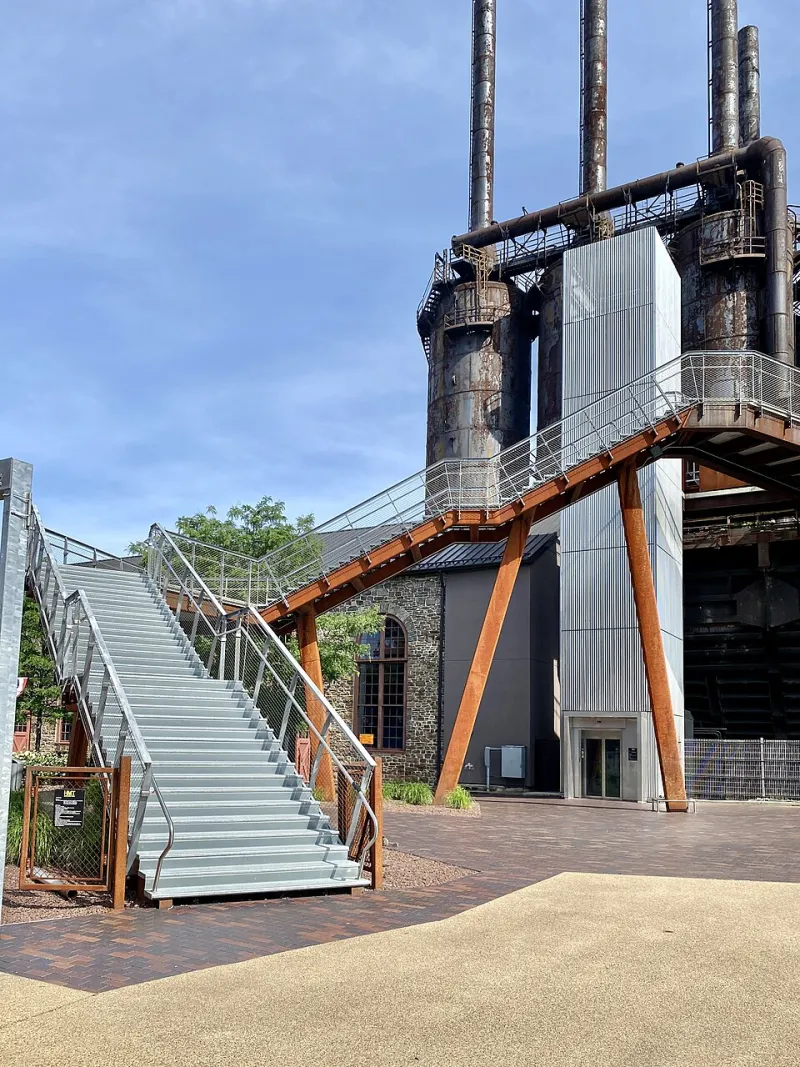
Photo: w_lemay, CC BY-SA 2.0, via Wikimedia Commons
A staircase that arrives with two flights of the same hand is not a fabrication failure in the ordinary sense. Every weld is sound, every dimension is within tolerance and every hole is where the drawing put it. The parts are simply the wrong way round, and because they are wrong in a way that only becomes obvious when they meet the building, the cost lands late: a return load, a crane standing idle, a site team sent home, and a pair of stringers that may or may not be salvageable depending on how much has already been drilled, welded and finished.
Handed work is routine in bespoke metalwork. Flights, balustrade panels, landing frames, gate leaves, access covers, bracketry and cladding returns all come in pairs or sets that differ only by orientation. Precisely because the difference is small, it is the class of error most likely to survive every check that is not specifically designed to catch it.
What the word hand is actually doing
The difficulty begins with language. A left-hand flight sounds definitive until two people discover they are describing it from opposite ends. One is thinking of standing at the bottom looking up; the other is thinking of the drawing sheet, where the flight runs left to right.
The workable discipline is to define hand by use rather than by appearance. On a stair, the convention that survives best is the one tied to ascent: state which side the handrail falls on when a person walks up the flight, and state the direction of that walk in terms of named floor levels or grid lines. Where a part is not a stair, tie the hand to an approach direction, a door swing, a hinge line or a designated primary elevation.
None of this matters unless it is written down. A convention held in the memory of a draughtsman is not a convention; it is a habit, and habits do not transfer to a night shift, a subcontracted profile cutter or a different fabricator picking up the repeat order in two years.
The traps in the drawing office
The first is the mirror command. Mirroring an assembly in a CAD environment is a single action, and it produces a result that looks entirely plausible on screen. What it may not do is carry across the annotations, the weld symbols, the part marks and the title-block descriptions with the same logic. A mirrored drawing that still says the original part number is a document waiting to mislead.
Second is the viewed-from direction. First-angle and third-angle projection place views differently on the sheet, and mixed or inherited templates can leave a view whose arrow has been moved or deleted. Where a view is relied upon to establish hand, the arrow and the label should be treated as part of the specification, not as decoration to be tidied away.
Third is the symmetrical-looking part. A frame with a central upstand may be handed only by the position of a single gusset, a cable entry or a drainage fall. If the drawing note reads opposite hand of item 12, the reader must find item 12, understand it, and invert it mentally. That is three steps where one would do.
Fourth is the revision trail. A pair issued at revision C, with one part reissued at revision D for a hole position, is no longer a guaranteed pair. The checking regime should treat the pair as a single deliverable with a single revision state.
Agreeing a convention that survives the workshop
A convention worth having is short enough to be printed on every relevant sheet and specific enough that it cannot be read two ways. It should identify the datum, the viewing direction, and the identifier for each member of the pair. Calling parts A and B, with a note that A is as viewed from the lower landing looking towards the upper, will do more work than any amount of left and right.
Three practical rules are worth adopting as standard:
- Never use left and right as the only descriptor on a drawing. Pair them with a datum and a direction, or replace them with part identifiers.
- State explicitly that the items form a handed pair and are not interchangeable. A note reading pair, do not interchange costs a line and prevents a substitution.
- Nominate one sheet, usually the general arrangement, as the authority for orientation, and make every component drawing refer back to it rather than restating the convention in its own words.
Marking that outlives the finish
A part that is correctly made but unmarked becomes a guess by the time it reaches the back of a van. Marking therefore needs the same attention as the joint preparation.
Consider what the part will endure before it is read on site: shot blasting, a zinc bath at around 450 degrees Celsius, a powder coat, a wrapping film, a stack of similar parts on top of it. Adhesive labels rarely survive all of that. Hard stamps, applied to a face that will not be seen in service, are more durable, but they must not be placed where they will interrupt a sealing face, a bearing surface or a specified finish.
Where hard stamping is prohibited, a combination works well: a durable tag wired to a dedicated lug, plus a paint or ink mark on a primed area in a fixed position, described on the drawing so that the next person knows where to look. Positional marking matters as much as the method. Top, outer face, 300mm up from the base is a location; a daub somewhere on the member is not.
The checks before loading
Trial assembly is the last point at which a reversed pair can be corrected cheaply, and it is worth planning rather than improvising. Where the parts are too large to assemble, a datum check on the bench will serve: lay both members out on the same orientation, confirm the handed features fall on opposite sides, and record the result with a photograph that shows the part marks in frame.
The loading sequence deserves its own check. Handed pairs should travel together, listed on the delivery note as a pair with their identifiers, and loaded so that the first item off the vehicle is the one the site needs first. A pair separated between two loads is a pair at risk.
For buyers, the questions to ask before work starts are straightforward. Who owns the orientation convention, and where is it written? Which drawing revision governs? What marking method has been agreed, and how will it survive the specified finish? Will there be a trial assembly, and will the evidence be provided? A fabricator who can answer those four questions without hesitation is a fabricator who has been caught out before and has fixed it.
Handed metalwork is not difficult to make. It is difficult to keep straight, and the difference between those two statements is entirely a matter of agreed language, visible marking and a check carried out at the right moment.